select
navigate
switch tabs
Esc close

sizing holes in sheet metal to receive PEM inserts

0
n
2

Hello all,

Xometry’s own design guidelines state that when PEM self clinching thread inserts are desired, one should refer to the insert manufacturer’s design guidelines.

The datasheet for the insert I’m interested in calls for a hole size of 5.41mm +0.08; Xometry on the other hand indicate that the kerf width for laser cutting is 0.2 – 0.4mm.

The range of possible kerf width is far too big to guarantee the hole comes out within tolerance.

Any advice?

Solved by Joao Clemencio
Hello, Great question, and you are absolutely right in your analysis. The +0.08 mm tolerance is indeed too tight to guarantee consistently with standard laser cutting alone due to the natural variation in the kerf width. To ensure your parts come out perfectly, we handle this in one of two ways, depending on how you prefer to receive your order: Option 1: Xometry installs the inserts for you: If you request us to supply and press the PEM inserts into the sheet metal, you don't need to worry about calculating the exact hole sizes or tolerances. What you need to do: Just provide a 2D technical drawing showing the sheet metal, the exact locations of the inserts, and the specific PEM part numbers/codes you require. Our manufacturing partners will take full responsibility for sizing the holes correctly and installing the inserts. Option 2: We supply the sheet metal, and you install the inserts yourself: If you prefer to order just the bare sheet metal and install the hardware on your end, we can still achieve that tight tolerance. To do this, our partners typically use secondary operations (like precision drilling or reaming after an undersized laser cut). What you need to do: You must attach a 2D technical drawing (PDF) alongside your 3D model. Call out the specific holes and explicitly indicate the required size and the +0.08 / -0.00 tolerance. The 2D drawing ensures our quality control team and manufacturing partners know exactly what strict tolerances must be met during fabrication. Both options are available through our platform. Let us know if you need any help setting up your quote!
    • n

      Hello all,

      Xometry’s own design guidelines state that when PEM self clinching thread inserts are desired, one should refer to the insert manufacturer’s design guidelines.

      The datasheet for the insert I’m interested in calls for a hole size of 5.41mm +0.08; Xometry on the other hand indicate that the kerf width for laser cutting is 0.2 – 0.4mm.

      The range of possible kerf width is far too big to guarantee the hole comes out within tolerance.

      Any advice?
      0
    • f

      Sort of been there…it’s one of those “let’s cover our back” cases where they state more conservative tolerances just in case

      We get several sheet metal parts with PEM inserts. Just state the tolerance clearly in you’re drawings. Had some other types of issues during prototyping (wrong inserts or bent) but none for being loose or fallen

      Technically these parts are assemblies, not just a “part”. I usually add a note next to the holes table like “All X holes have a Tolerance of +/-Y”. Unless there aren’t that may holes/inserts, then it’s just a Tol call out on the dimension itself

      We’ve even had cases of repeating orders where they come back saying “this tolerance is too tight for the process”, and I’m like “Brother, you’ve done it before. Why is it an issue now?”. No answer back and part arrives just fine 🙂

      0
      Reply
    • n

      Thanks! So to clarify, you’re saying that PEM indicate an overly conservative tolerance for the hole size, and the hole itself can actually be materially larger?


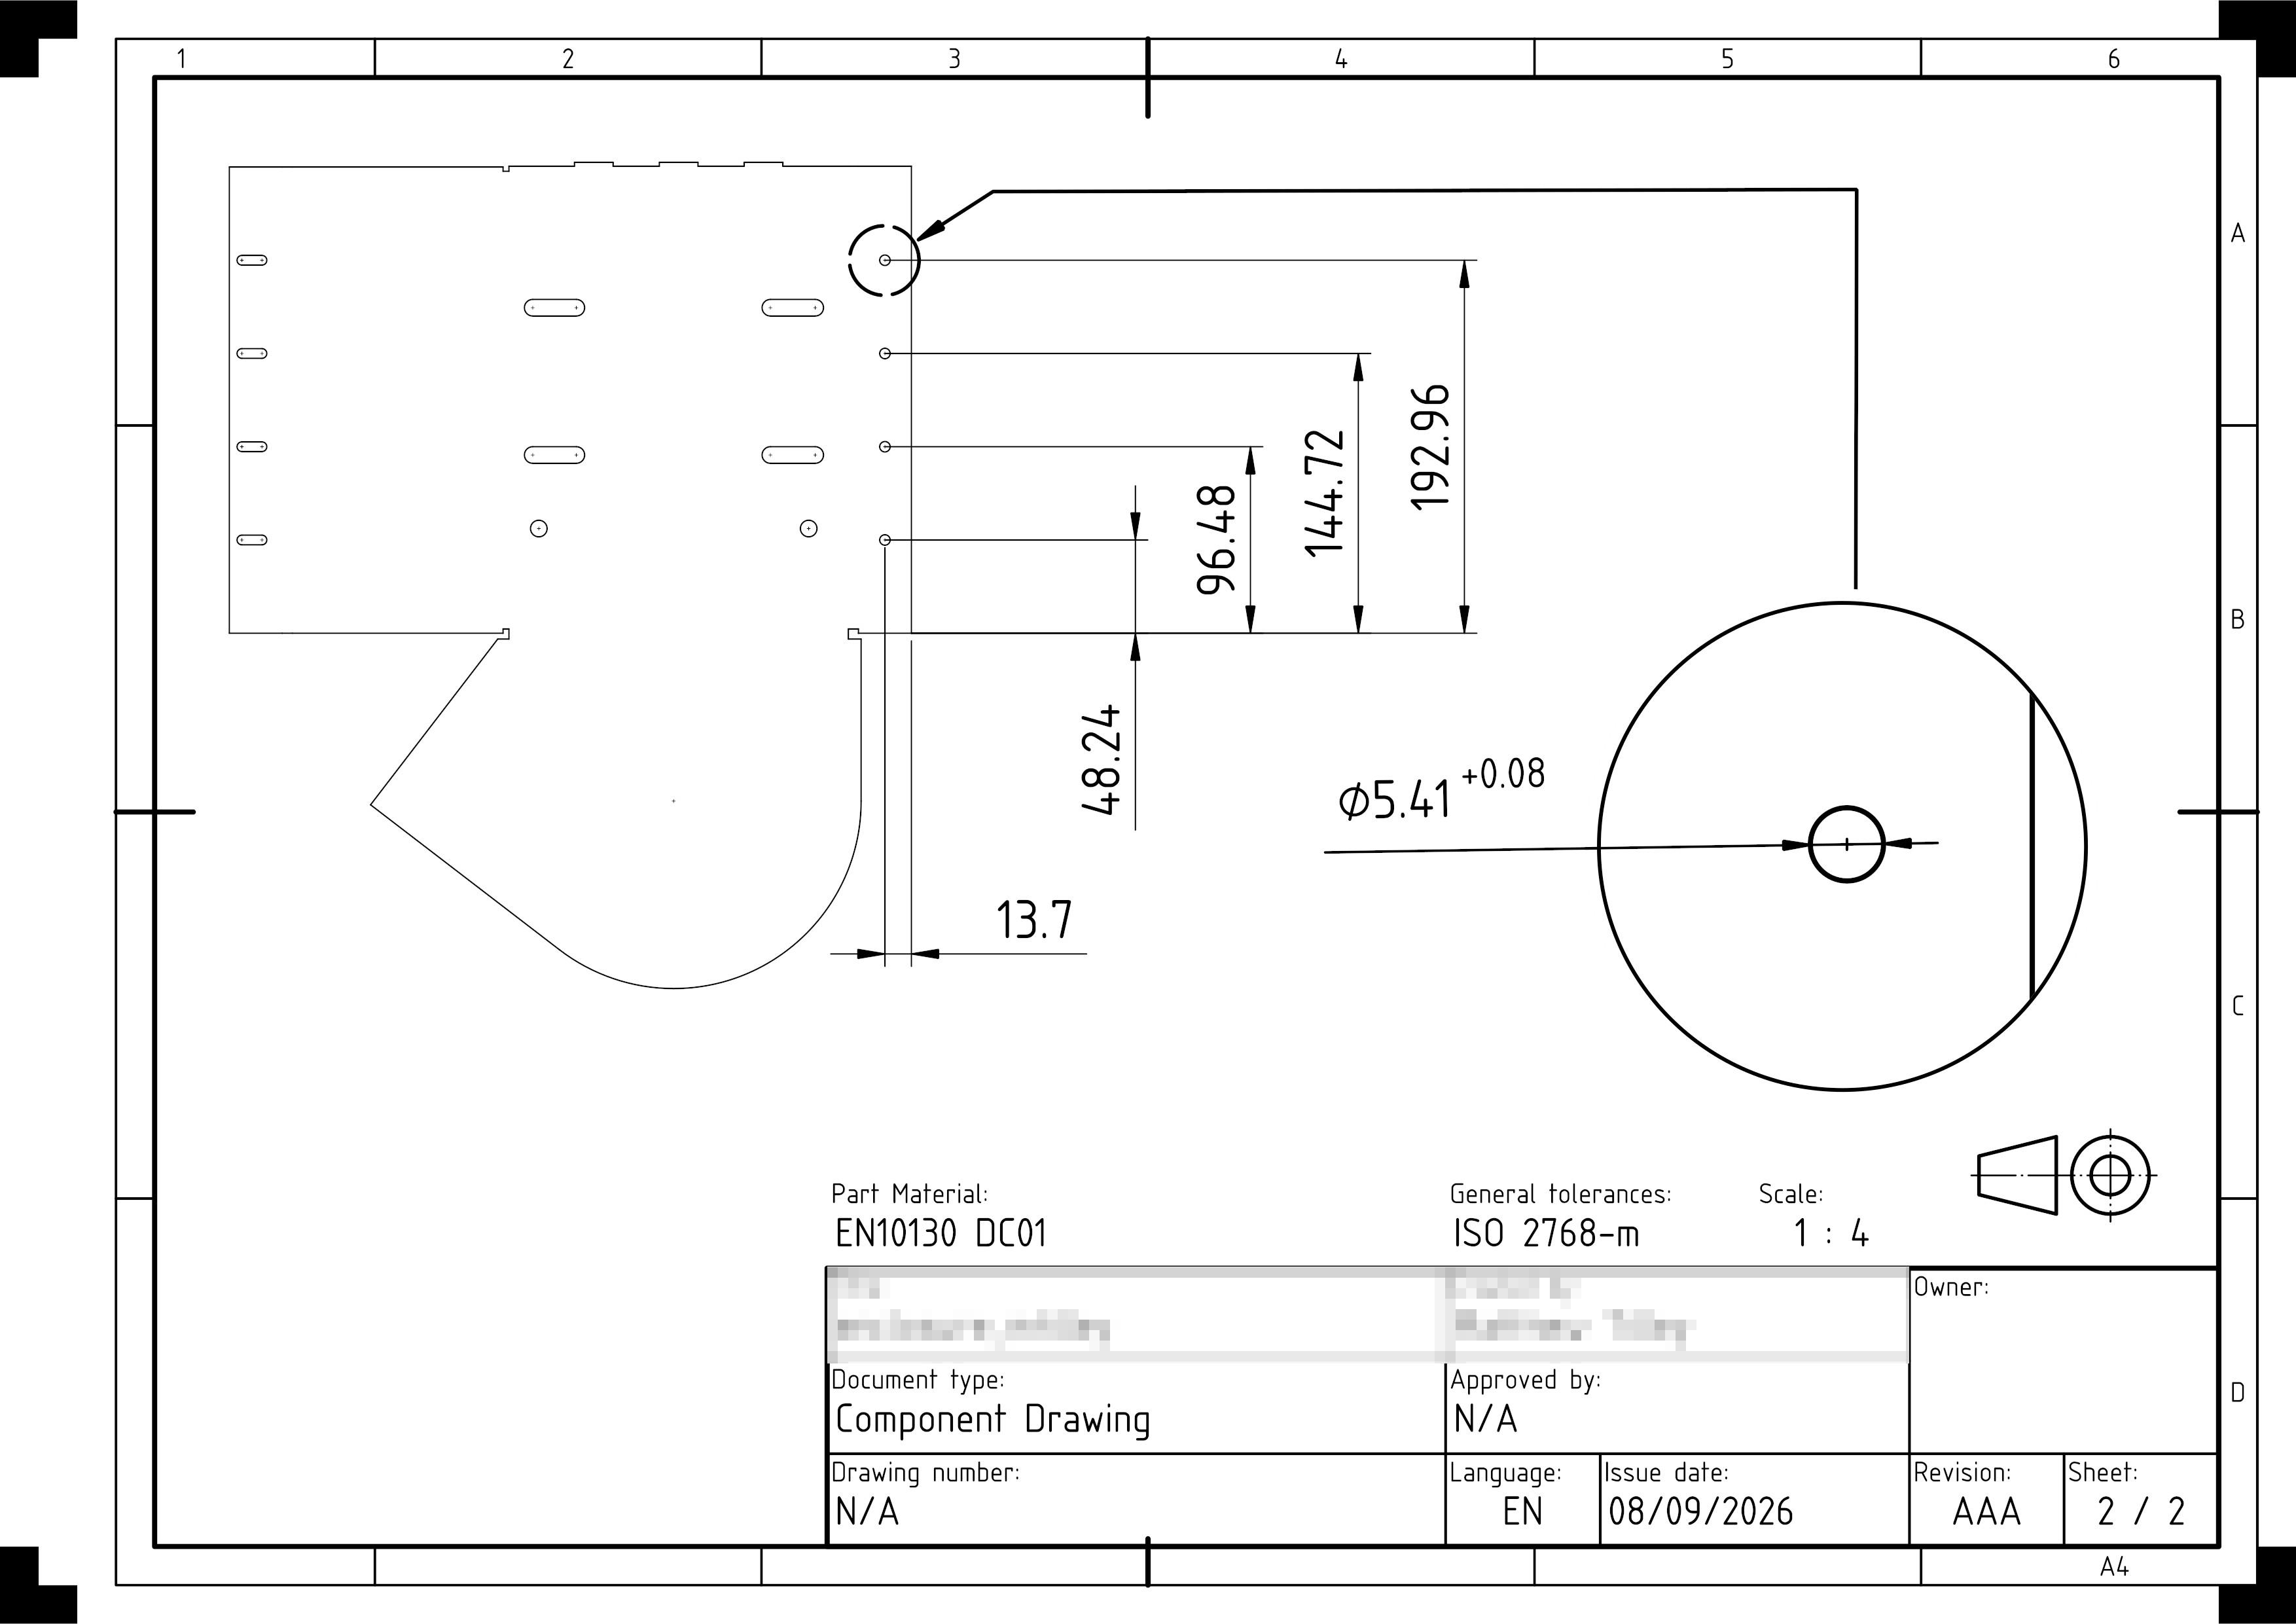
      The issue is that if the tolerance is too narrow to be held by laser cutting, I’ll need to remove the holes in question from my .dxf file and instead define them in the drawing; they would need drilling. But, in all of the material I’ve read through on designing for laser cutting, nowhere have I seen any suggestion that laser cut holes can’t reliably be used to install PEM inserts.


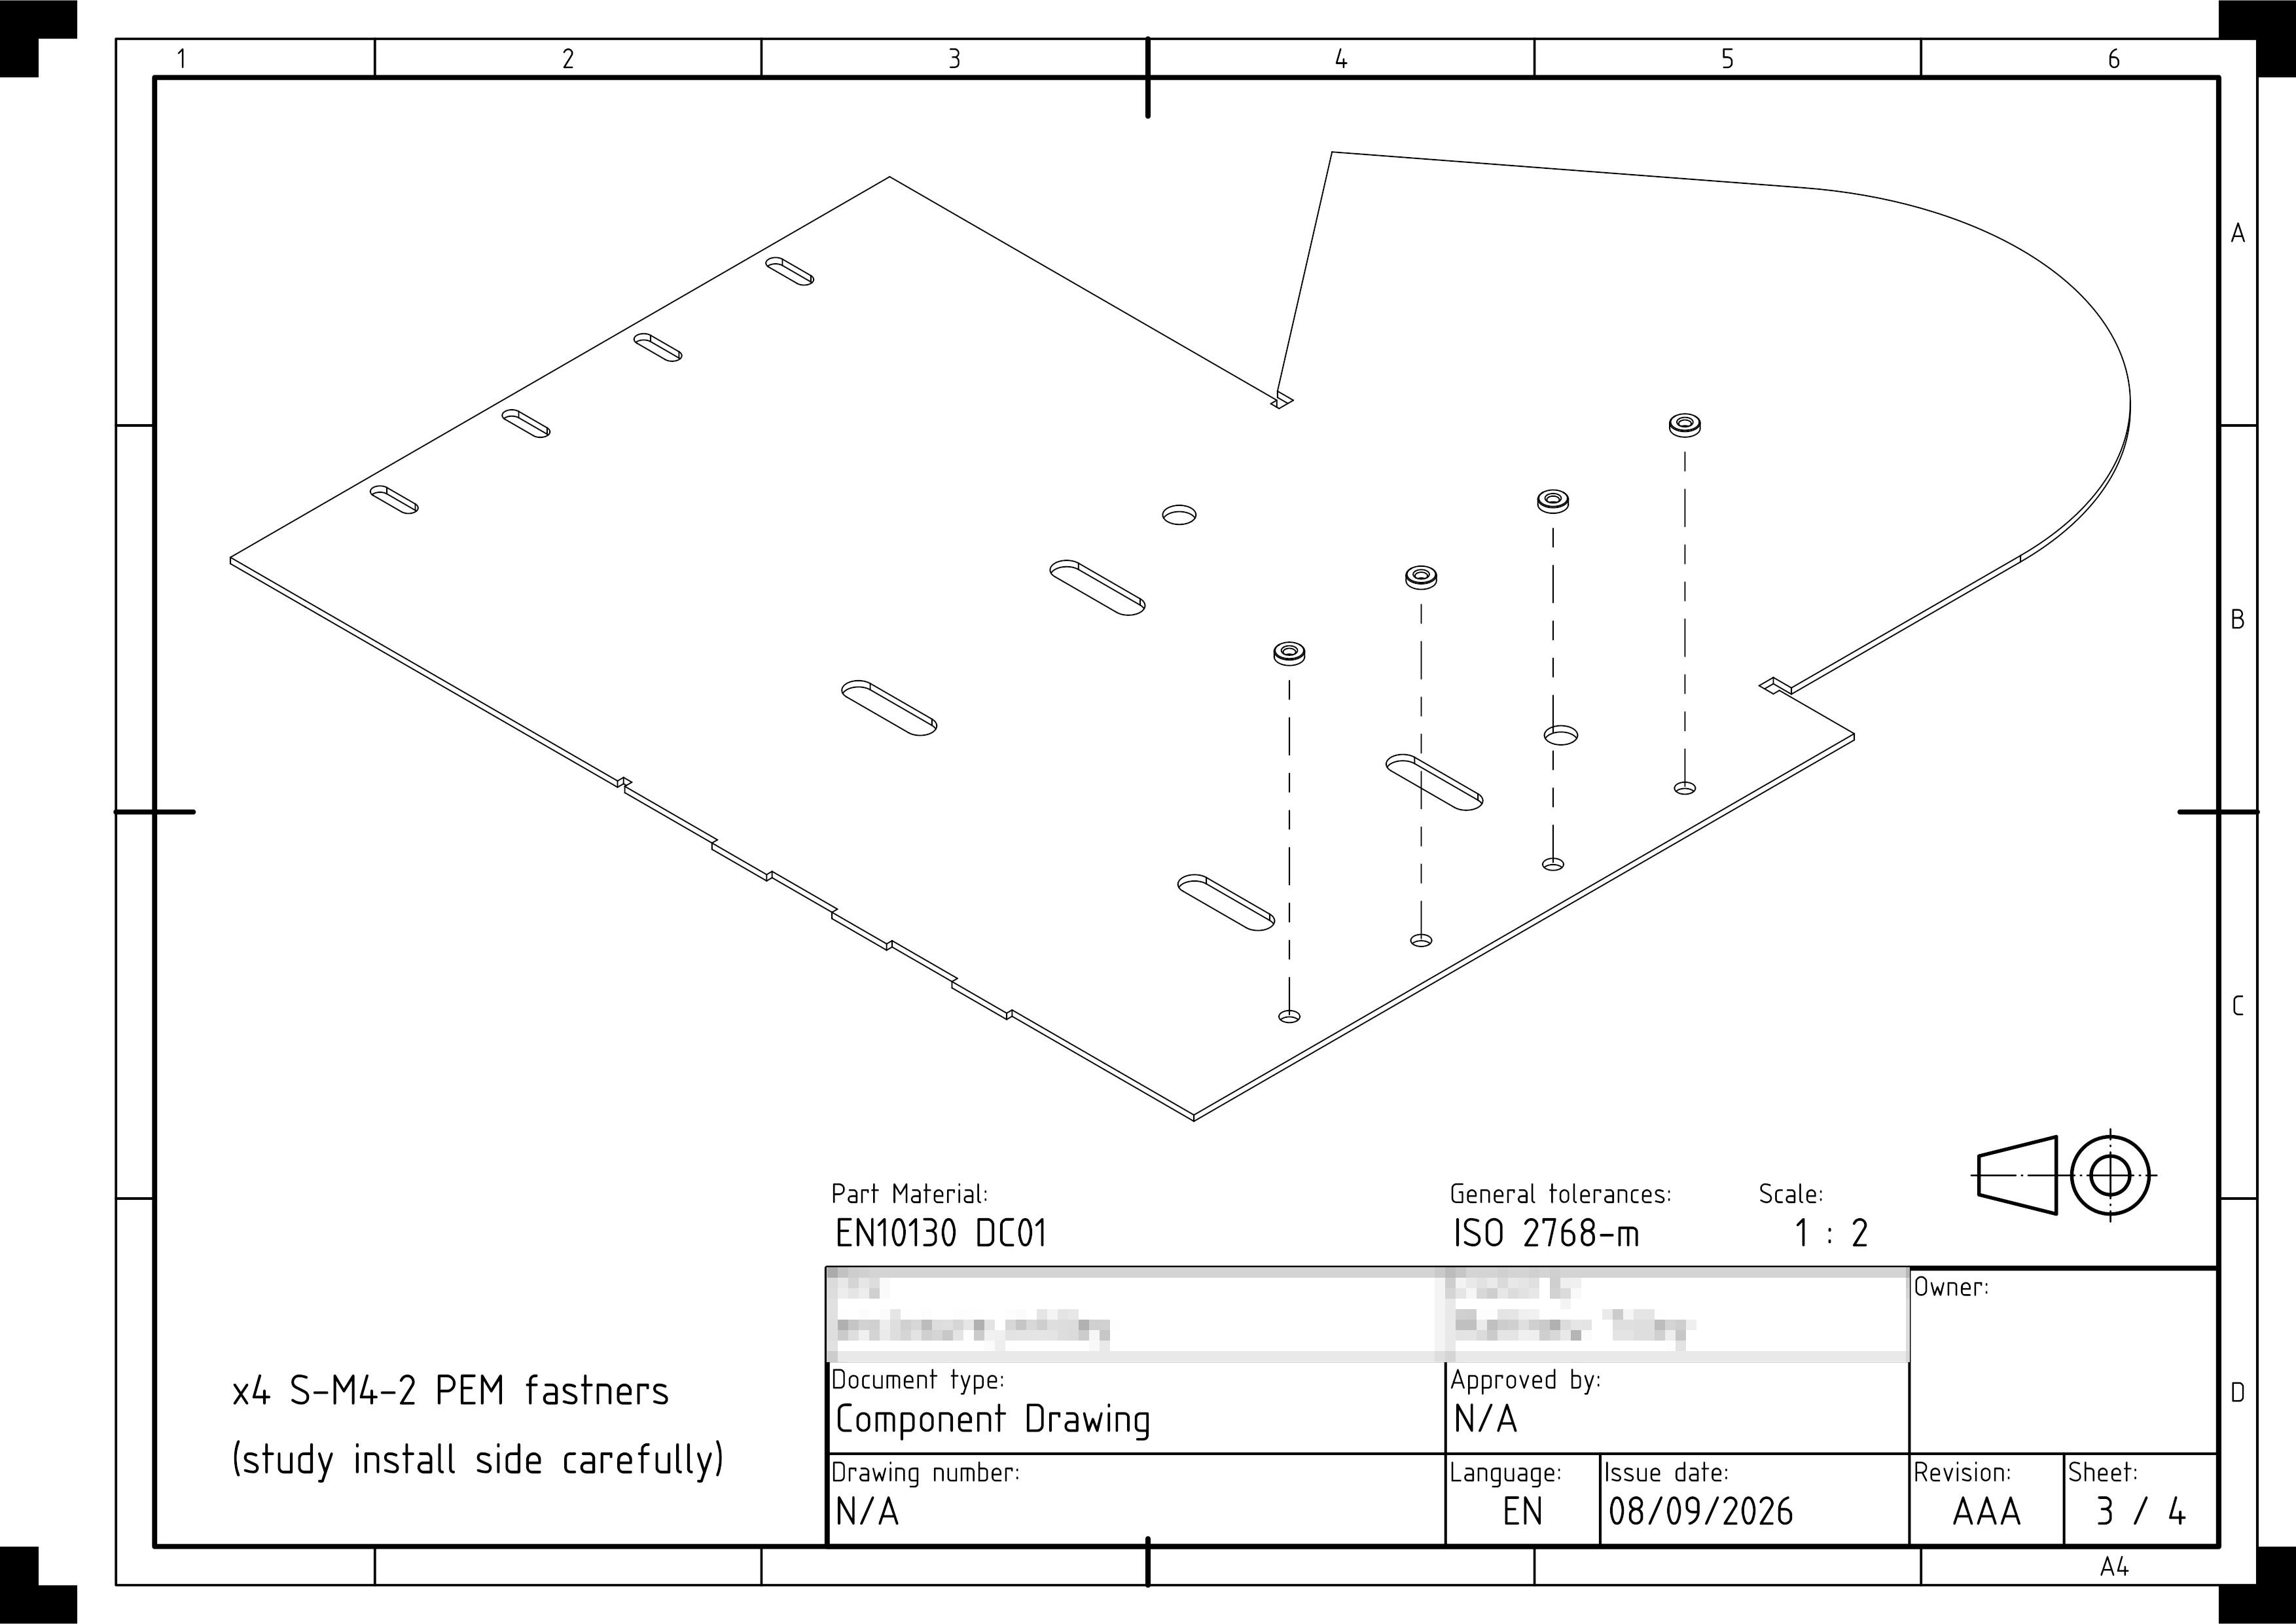
      I’ve included a couple of pages from the drawing below so it can be seen what I’m going for.


      0
      Reply
    • Xometry Engineer

      Hello,

      Great question, and you are absolutely right in your analysis. The +0.08 mm tolerance is indeed too tight to guarantee consistently with standard laser cutting alone due to the natural variation in the kerf width.

      To ensure your parts come out perfectly, we handle this in one of two ways, depending on how you prefer to receive your order:

      Option 1: Xometry installs the inserts for you:

      If you request us to supply and press the PEM inserts into the sheet metal, you don’t need to worry about calculating the exact hole sizes or tolerances.

      What you need to do: Just provide a 2D technical drawing showing the sheet metal, the exact locations of the inserts, and the specific PEM part numbers/codes you require. Our manufacturing partners will take full responsibility for sizing the holes correctly and installing the inserts.
      Option 2: We supply the sheet metal, and you install the inserts yourself:

      If you prefer to order just the bare sheet metal and install the hardware on your end, we can still achieve that tight tolerance. To do this, our partners typically use secondary operations (like precision drilling or reaming after an undersized laser cut).

      What you need to do: You must attach a 2D technical drawing (PDF) alongside your 3D model. Call out the specific holes and explicitly indicate the required size and the +0.08 / -0.00 tolerance. The 2D drawing ensures our quality control team and manufacturing partners know exactly what strict tolerances must be met during fabrication.
      Both options are available through our platform. Let us know if you need any help setting up your quote!

      0
      Reply
sizing holes in sheet metal to receive PEM inserts
Your information:


Suggested Topics

Topic
Replies
Views
Activity
Contact
Good day, I have been trying to receive the materials I paid for, for several days now. It's impossible to speak with anyone who can provide a serious and reliable update. The service is... read more
c
2
149
Aug 25
3D Printing
Good morning, I would like a quote. I have attached some photos of 3D designs already created with AutoCAD as solids. I also have the DWG file that you can reference or use as... read more
l
1
137
Aug 20
Request for Material Information for Trumpet Mouthpiece
Good day. I have a trumpet mouthpiece that I have modeled myself using FreeCAD, which I need to print. I conducted a small research and Google suggests using PETG (Polyethylene Terephthalate Glycol-modified) as a... read more
m
6
226
Jul 29
DMLS AlSi10Mg – Surface Finish Optimization & Leak-Proofing Methods
Hi everyone, I’m working with DMLS (AlSi10Mg) and looking for advice on post-processing. What finishing methods do you recommend to achieve a smooth (non-grainy) surface, especially for functional parts? Also, what’s the best approach... read more
p
1
810
Mar 27